Hot vulcanizing, cold bonding or mechanical fasteners: which joint?
- Share
- Issue Time
- Oct 20,2026
Short answer: hot vulcanizing gives the strongest, smoothest and longest-lasting joint but needs a press, power and skilled labor; cold bonding uses adhesive and cures at room temperature — faster and tool-light, but generally weaker than a hot splice; mechanical fasteners are the fastest emergency fix with the lowest joint strength. For permanent installations choose hot vulcanizing; use cold bond or fasteners for time-critical repairs.
Three joint methods compared
| Criterion | Hot vulcanizing | Cold bonding | Mechanical fasteners |
|---|---|---|---|
| Joint strength | Highest — typically around 70–90% of base belt | Good, generally below hot splice | Lowest — holes weaken the belt |
| Equipment needed | Vulcanizing press, power source | Adhesive kit, basic hand tools | Fastener tool, hand tools |
| Working time | Hours (heat-up and curing cycle) | About an hour plus adhesive cure | Minutes |
| Surface finish | Smooth and continuous | Near-smooth | Protruding bumps |
| Skill required | Trained splicer | Moderate | Minimal |
| Best for | Permanent installs, high-tension drives | Repairs without press access, moderate loads | Emergency restarts, temporary service |
When hot vulcanizing is worth it
- The belt runs at high tension or transmits significant power where a weak joint would creep or fail.
- The installation is long-term — joint life matters more than joint speed.
- Product contacts the belt surface and bumps from fasteners would mark it or catch scrapers.
When cold bond or fasteners make sense
- The production line is down and every hour costs more than joint longevity — fasteners get you running today.
- No press or power is available on site; a cold bond is the strongest tool-light option.
- The belt is a low-tension, light-duty conveyor where joint strength demand is modest.
Whichever method you choose, joint preparation quality decides the result: clean and dry ends, correct cut pattern, accurate alignment and full curing. A rushed splice of any type fails early. Values above are industry-general guidance; confirm the method against your belt type and tension rating.
Not sure which joint suits your line?
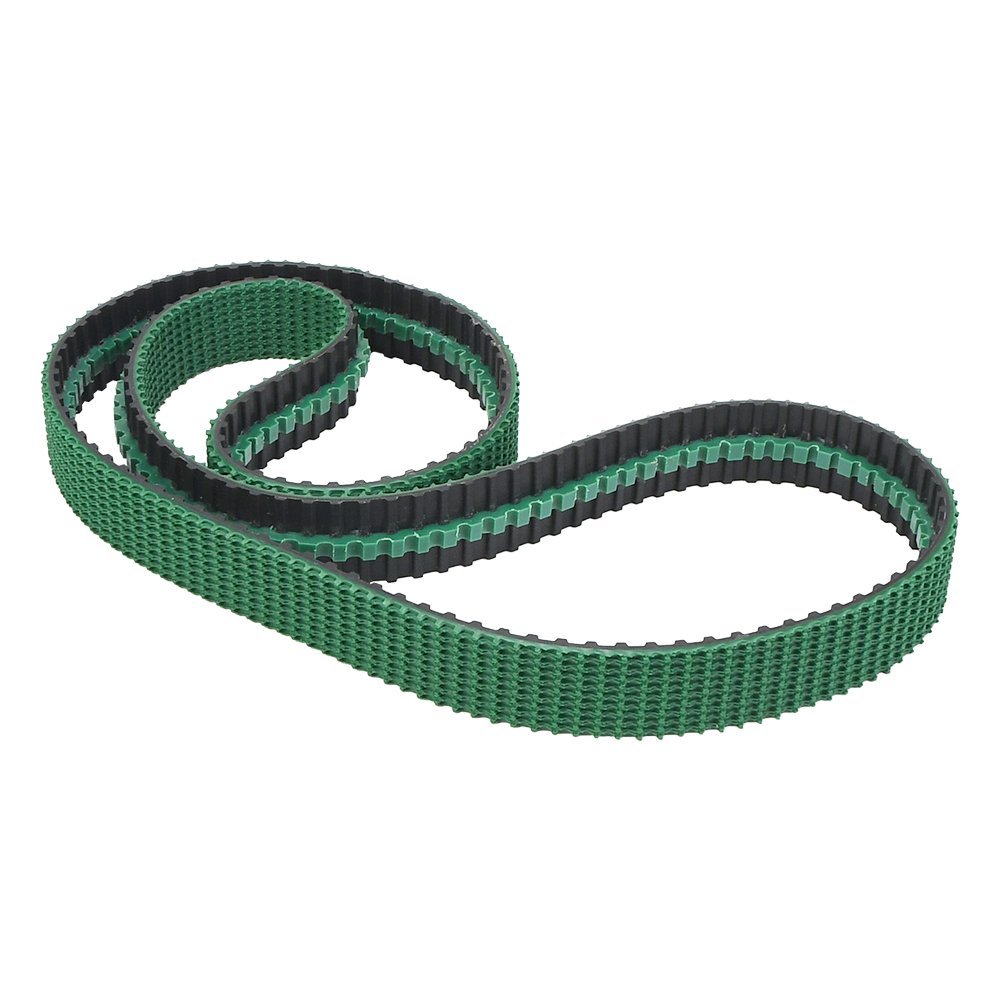
Tell us the belt type, tension level and site conditions — we will recommend the joint method and supply material, tooling or ready-made endless belts.
Ask for Joint Advice